China Top Custom Zinc Alloy Die Casting Manufacturer
China’s manufacturing strength is changing how global buyers evaluate Custom Zinc Alloy Die Casting. Price still matters, but it no longer tells the whole story. Consistent dimensions, clean surfaces, and dependable delivery matter more.
Dr. Frank C. Goodwin, a recognized zinc-industry specialist, has stated, “Zinc combines precision, productivity, and recyclability when its process is controlled.” That principle reflects real production conditions. A skilled manufacturer checks alloy composition, mold temperature, injection speed, and filling pressure. Small changes can affect porosity, flash, and surface texture. A thin phone bracket may require different controls than a heavy automotive housing. Details decide performance.
The best Chinese suppliers connect engineering support with disciplined factory work. They review 3D drawings, identify difficult corners, and recommend practical wall thicknesses. They also inspect first articles before full production. This reduces expensive surprises. Traceable material records and dimensional reports add confidence for international customers. The process should include pressure testing, visual checks, and sampling plans when the component requires them.
No factory gets every shot perfect. That is the uncomfortable truth. Even experienced teams can miss a minor burr or underestimate a coating issue. Reliable manufacturers respond with corrective action, not vague promises. Buyers should ask about tooling life, zinc alloy grades, quality certificates, packaging methods, and after-sales support. Custom Zinc Alloy Die Casting is not merely a casting service. It is a controlled partnership between design, tooling, production, and inspection. When those parts work together, a China-based supplier can deliver precise components with competitive value and repeatable quality.
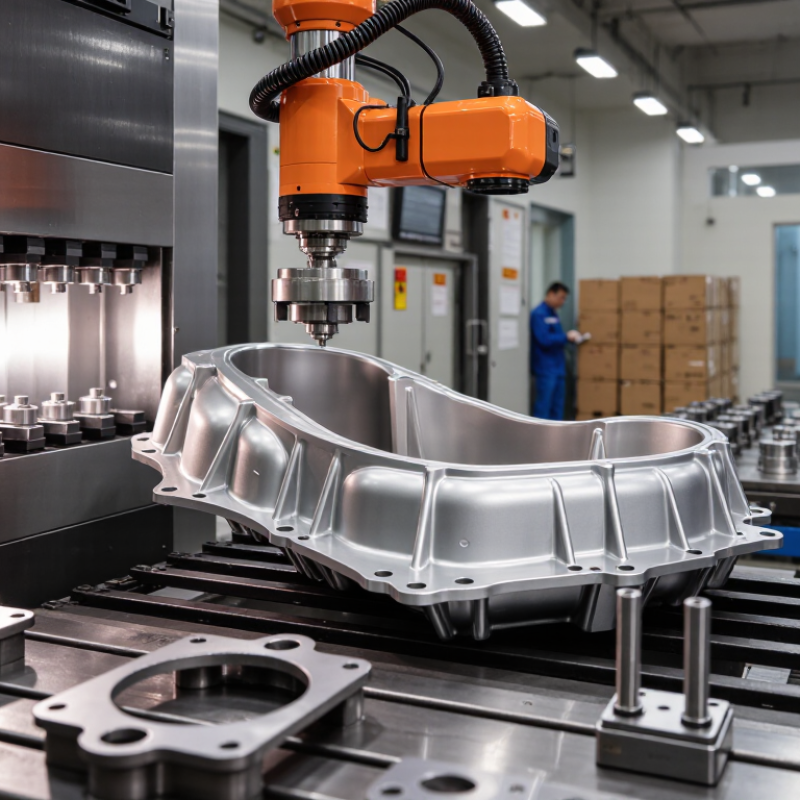
China’s Custom Zinc Alloy Die Casting Manufacturing Overview
China Top Custom Zinc Alloy Die Casting Manufacturer
China’s Custom Zinc Alloy Die Casting Manufacturing Overview
China has a mature zinc alloy die casting supply chain, supported by mold makers, casting plants, and finishing workshops. Custom production usually begins with a 3D design review and flow simulation. Engineers check wall thickness, draft angles, ejector locations, and likely air entrapment before cutting the mold.
Hot-chamber machines are common for zinc alloys because they support fast, repeatable cycles. Zinc flows into detailed cavities and can produce thin walls, textured surfaces, and clean threads. After casting, parts may receive trimming, drilling, polishing, plating, or powder coating. A dependable manufacturer records melt temperature, injection pressure, cycle time, and dimensional results. These records help explain variation instead of hiding it.
Tips: Share the 3D file, material grade, annual quantity, and surface expectations early. Ask for first-article samples and a written inspection plan. Small design changes can reduce flash and extend mold life. Do not judge a supplier by equipment size alone. Communication, traceability, and corrective action matter more than impressive photographs.
Cost remains important, but low tooling prices can create later problems. Poor venting may leave pinholes or weak edges. Uneven cooling can cause distortion. No process is flawless. Experienced teams still review rejected samples, question assumptions, and improve the next production run. For overseas buyers, clear packaging details and pre-shipment inspection also protect consistency during delivery.
Zinc Alloy Materials and Their Die Casting Advantages
China Top Custom Zinc Alloy Die Casting Manufacturer
Zinc Alloy Materials and Their Die Casting Advantages
Zinc alloy is valued for its balanced strength, fluidity, and surface quality. It commonly contains zinc with controlled amounts of aluminum, magnesium, and copper. This composition helps molten metal fill detailed cavities quickly. Fine ribs, threads, logos, and narrow walls can often be formed directly in the mold.
The material also supports repeatable production. Zinc alloy flows at relatively low temperatures, reducing thermal stress on tooling and shortening casting cycles. Its density gives parts a solid, substantial feel without requiring excessive wall thickness. After casting, surfaces can receive polishing, plating, powder coating, or painting. These options suit handles, housings, fittings, and precision hardware.
Production experience still matters. A well-designed mold cannot correct poor venting or unstable alloy control. Engineers should review draft angles, gate locations, cooling paths, and expected loads before cutting steel. Zinc alloy offers good dimensional accuracy, but thin sections may warp when cooling conditions are uneven. That detail is easy to underestimate.
Quality checks should include alloy composition, hardness, dimensions, porosity, and coating adhesion. Samples from different production stages reveal process drift more reliably than one final inspection. Zinc alloy is also recyclable, although mixed coatings and attached materials require proper separation. Sometimes, a lighter alloy may be better. Material selection should follow the part’s function, service environment, and production volume rather than appearance alone.
Zinc Alloy Materials and Their Die Casting Advantages
The chart compares typical ultimate tensile strength values for common Zamak zinc alloys used in die casting. Zinc alloys provide excellent fluidity, good dimensional accuracy, thin-wall capability, high recyclability, and strong surface finishing performance. Values are typical room-temperature properties and may vary with casting design, heat treatment, and applicable material standards.
Custom Die Casting Process from Design to Finished Parts
China Top Custom Zinc Alloy Die Casting Manufacturer
Custom die casting begins with a practical design review, not a machine cycle. Engineers study wall thickness, draft angles, ribs, holes, and assembly requirements. Zinc alloy can fill detailed cavities, but sharp corners may create stress or uneven flow. Small errors grow.
The team converts approved drawings into tool designs and checks filling behavior through simulation. Mold steel selection, gate location, cooling channels, and ejection points affect part quality. A trial mold then produces sample parts for measurement and visual inspection. That step matters. Dimensions are checked with calibrated gauges, while surfaces are examined for flash, pores, scratches, and incomplete filling.
After approval, production runs under controlled pressure, temperature, and cycle time. Operators monitor these settings because stable conditions support repeatable results. Parts may receive trimming, deburring, polishing, plating, painting, or protective coating. Each operation needs clear acceptance criteria. Traceable inspection records also connect material batches, machine settings, and final measurements.
Practical experience shows that drawings do not reveal every manufacturing risk. A part may pass dimensional checks but still feel weak during assembly. Another may look attractive but require excessive finishing. Reviewing these issues early improves the next design. Honest feedback, documented process changes, and consistent inspection build dependable custom zinc alloy die cast parts from concept to shipment.
Manufacturer Capabilities, Quality Control, and Certification
Custom zinc alloy die casting demands more than fast cycle times. A capable manufacturer should control tooling, melting, injection, trimming, and finishing under one documented process. USGS Mineral Commodity Summaries 2024 estimated global zinc mine production at about 12 million metric tons in 2023. Stable material sourcing still matters, especially when alloy chemistry affects strength, porosity, and surface appearance.
Quality control should begin before the first shot. Engineers can review wall thickness, draft angles, gate locations, and shrinkage risks using simulation. Operators should verify furnace temperature and alloy composition. CMM inspection, X-ray sampling, thread gauges, and coating tests help confirm dimensional and cosmetic requirements. The 2023 ISO Survey recorded more than 1.26 million ISO 9001 certificates worldwide. Certification is useful, but it is not proof of perfect production. Ask for the certificate scope, audit date, and inspection records.
Environmental and automotive projects may require ISO 14001 or IATF 16949 systems. These standards support traceability, corrective action, and controlled supplier management. A reliable factory should provide material certificates, first-article reports, control plans, and batch identification. Details matter. A missed burr can stop assembly. Some inspections remain sample-based, so risk-based testing should be agreed before production. Even experienced teams need review; process capability can drift after tooling repair, operator changes, or recycled-material adjustments.
How to Choose a Reliable Chinese Zinc Alloy Die Casting Partner
China Top Custom Zinc Alloy Die Casting Manufacturer
How to Choose a Reliable Chinese Zinc Alloy Die Casting Partner
Choosing a reliable Chinese zinc alloy die casting partner starts with process evidence, not polished photographs. Ask how engineers select alloy grades, gate locations, and draft angles for your part. A capable team should explain porosity risks, dimensional shrinkage, and surface finishing limits. Request trial samples from production-intent tooling. Details matter. Review inspection records for dimensions, weight, appearance, and critical threads.
Factory experience becomes visible during difficult conversations. Ask what happens when flash appears near a sealing surface or a cavity fills unevenly. The answer should include root-cause analysis, corrective actions, and updated process controls. Confirm whether the supplier uses coordinate measuring machines, alloy testing, and documented first-article inspections. For high-risk components, discuss X-ray inspection and traceability by batch. Ask for evidence.
A dependable partner also communicates clearly before tooling begins. Require written tolerances, mold ownership terms, sample approval steps, packaging details, and delivery milestones. Check whether project engineers can review drawings in your working language and report changes promptly. Independent audits can reveal housekeeping, maintenance habits, and actual production capacity. Do not choose by price alone; an inexpensive mold can create expensive revisions. I have seen teams approve attractive samples too quickly, then discover inconsistent threads in volume production. That mistake is preventable, but not always. Select a supplier willing to show limitations, not only confidence.
| Evaluation Dimension | Industry-Based Data or Recommended Benchmark | Why It Matters | Verification Method | Priority |
|---|---|---|---|---|
| Material Identification | Common zinc die-casting alloys include Zamak 3, Zamak 5 and ZA-8. Typical zinc alloy density is approximately 6.6–6.7 g/cm³. | The alloy grade affects strength, ductility, dimensional stability, corrosion resistance and surface finishing performance. | Request the material designation, chemical composition report and a batch-based material certificate. | Critical |
| Mechanical Performance | Typical ultimate tensile strength varies by alloy and condition; Zamak 3 and Zamak 5 are commonly specified in the approximate range of 280–330 MPa. | Mechanical requirements must match the part’s load, impact, wear and service-life conditions. | Review alloy-specific technical data and verify production samples through an independent or accredited laboratory when required. | Critical |
| Dimensional Capability | Die casting can produce thin-wall components and repeatable dimensions, but achievable tolerances depend on part size, geometry, tooling design and measurement method. | Clear tolerances prevent disputes and reduce machining, assembly and rejection costs. | Provide a fully dimensioned drawing with GD&T, datum references and inspection points; review a first-article inspection report. | Critical |
| Applicable Standards | Use recognized casting and geometric tolerancing references, such as ISO 8062 for cast products and ISO 2768 where applicable to general tolerances. | Standards create a common technical language for drawings, inspection and acceptance criteria. | Confirm the standards listed on the quotation, drawings, control plan and inspection report. | High |
| Mold and Tooling Plan | Tooling life depends on alloy, shot parameters, mold steel, part geometry, maintenance and production volume; it should be defined contractually rather than assumed. | A documented tooling plan reduces unexpected repair charges and production interruptions. | Ask for mold-flow review, tool design approval, maintenance intervals, ownership terms and a repair or replacement policy. | Critical |
| Machine Capacity | The selected die-casting machine must provide sufficient locking force, shot volume, die dimensions and ejection capacity for the part and mold. | Incorrect machine selection can cause flash, incomplete filling, porosity, deformation or unstable cycle times. | Request the machine tonnage, shot-weight range, tie-bar spacing, maximum mold dimensions and equipment maintenance records. | Critical |
| Production Process Control | A controlled process normally includes documented parameters for melting, die temperature, injection speed, pressure, cycle time, trimming and inspection. | Stable process parameters are essential for repeatable quality across batches. | Review the process flow chart, control plan, work instructions, process records and corrective-action procedure. | Critical |
| Internal Quality Systems | A mature supplier should operate documented quality procedures, traceability and nonconformance controls; certification to ISO 9001 is a useful verification point. | Quality systems reduce variation and make root-cause investigation more reliable. | Check the current certificate scope and validity, audit the facility and review sample inspection records. | High |
| Porosity and Defect Control | Common die-casting defects include gas porosity, shrinkage, cold shuts, flow marks, flash and inclusions. Acceptance limits must be defined for each part. | Internal defects may reduce pressure tightness, strength, plating quality and long-term reliability. | Specify visual limits, cross-section requirements, leak testing or X-ray inspection when the application requires it. | Critical |
| Surface Finishing | Zinc alloy parts can commonly receive polishing, painting, powder coating, electroplating or passivation, subject to alloy and surface preparation. | Finishing affects appearance, corrosion resistance, wear resistance and customer acceptance. | Approve signed reference samples and define coating thickness, color tolerance, adhesion, corrosion and appearance criteria. | High |
| Testing and Inspection Equipment | Suitable equipment may include calibrated calipers, CMMs, spectrometers, coating-thickness gauges, hardness testers and leak-test equipment. | Capability to measure critical characteristics is more reliable than visual assurances alone. | Review equipment lists, calibration certificates, measurement-system records and sample inspection data. | High |
| Traceability | Production records should link raw material, mold, machine, operator, production date, inspection results and shipment batch. | Traceability supports rapid containment, warranty analysis and regulatory documentation. | Request a redacted example of a batch traveler, material record and final inspection report. | High |
| Prototype and Sampling | Before mass production, approve samples for dimensions, function, appearance, material and finishing using the same process intended for production. | Production-intent samples reveal tooling and process risks earlier than quotation-stage discussions. | Use a signed sample approval record and a first-article report covering all critical characteristics. | Critical |
| Packaging and Logistics | Packaging should prevent scratching, deformation, oxidation and contamination during handling and international transport. | Good packaging protects finished surfaces and reduces transit-related claims. | Approve packaging drawings or photographs and define carton quantity, labeling, palletization and shipping documents. | Medium |
| Commercial Transparency | A complete quotation should separate tooling, part price, finishing, inspection, packaging, freight assumptions, payment terms and lead times. | Transparent pricing makes suppliers comparable and limits unexpected charges. | Compare itemized quotations and confirm inclusions, exclusions, tooling ownership and engineering-change charges in writing. | High |
| Supplier Audit Readiness | A reliable partner should be able to provide facility access or a structured remote audit covering production, quality, storage and subcontracted finishing. | Audits verify whether quoted capabilities are supported by actual equipment and procedures. | Use a documented audit checklist and record objective evidence, open actions and completion dates. | High |
| Note: Performance ranges are indicative industry references, not universal acceptance limits. Final requirements should be defined by the approved drawing, material specification, applicable standards and validated inspection plan. | ||||